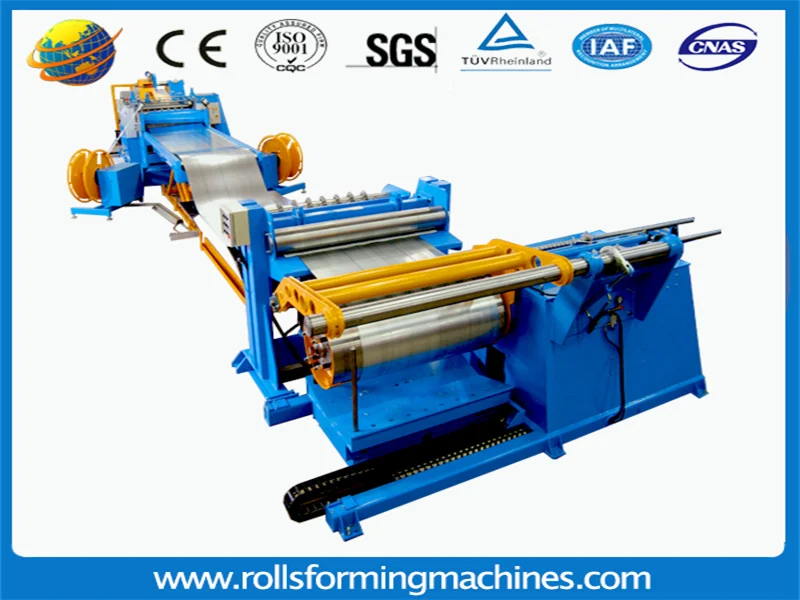
The ZT-4×1500 Hydraulic Slitting Line converts one master steel coil up to 15 t into multiple precision strips in a single pass — uncoiling, pinch feeding, slitting, edge scrap winding, tensioning and recoiling on one continuous line.
It processes carbon steel 1.5–4 mm and stainless steel 1.5–2.5 mm, master coil width 500–1500 mm, at line speed up to 40 m/min, with strip width tolerance held within ±0.1 mm. One 1500 mm master coil can be slit into 15 strips at 1.5 mm, 10 strips at 2 mm, 7 strips at 3 mm or 6 strips at 4 mm — with a minimum finished strip width of 30 mm.(Quantity of strips at one time (Max for carbon steel))
The line is driven by a 75 kW AC slitting motor and a 90 kW AC recoiler on PLC frequency-conversion control. Two hydraulic loops and a tension stand with dividing shafts work with the recoiler to produce tight, even coils. with Siemens PLC, Schneider and CHNT electrical components, and a complete tooling package including 20 LD slitting blades.
Working Process
Line direction: from right to left; the operation table faces the machines.
- Hydraulic entry coil car — hydraulic lifting with 4 guide pillars and cycloid-motor traverse at 6–7 m/min. Capacity 15 t. Loads the coil onto the decoiler mandrel and returns part-processed coils to the start position. Controlled from the auxiliary panel.
- Hydraulic decoiler — wedge-type hydraulic expand/shrink mandrel, Φ520 max / Φ480 min × 1500 mm, coil weight up to 15 t, with hydraulic supporting arm and brake. The 1.5 kW cycloid reducer drives the press arm.
- Hydraulic press, pinch and pre-leveler device — hydraulic shovel head and press head for coil opening and feeding. 15 kW cycloid reducer motor drives the pinch rollers, which are lifted by motor or adjusted by hand wheel. Unit consists of the drive, 2 pinch rollers, 5 leveling rollers and frame.
- Hydraulic head cutter — double-column structure, shears 4 mm × 1500 mm plate. LD alloy blades with adjustable upper/lower clearance. Trims the coil head for smooth entry into the slitter and can cut a large coil into small coils.
- Loop I — hydraulic lifting roller table. Pit size 3500 × 2000 × 3500 mm.
- Side guide (centering) unit — frame, guide rods, adjustment mechanism, movable platform and multi-roller wheels. Vertical guide rollers on both sides, adjusted by hand wheel and both-end screws, width range 500–1500 mm.
- Slitting machine (75 kW AC) — blade shaft Φ220 mm in 40Cr, blades Φ360 × Φ220 × 15 mm in LD material, frequency-conversion speed control with cycloidal reducer. Side guides position the strip and stop strip jumping to improve slitting accuracy. Active shearing and pull shearing are switchable to meet the accuracy requirements of different strip thicknesses.
- Scrap winder (4 kW) — winds the edge trim produced by slitting. Consists of base, scrap shaft, scrap plate, friction wheel, chain drive and reducer.
- Loop II — hydraulic lifting roller table. Pit size 4000 × 2000 × 5000 mm.
- Tension stand with cutter — welded steel plate frame, pre-dividing shaft, housings, press shaft with hydraulic damp device and hydraulic lifting/pressing mechanism, divider plates and spacers, plus a hydraulic transition table for easy strip passage. It guides the finished strips left and right, prevents deviation, and builds tension with the recoiler to keep recoiled coils tight and even.
- Recoiler (90 kW AC) — hydraulic expand/shrink mandrel Φ508 × 1500 mm, coil weight up to 15 t with hydraulic supporting arm, JZQ650 reducer (i = 40.17), integral steel plate cantilever structure. Works with first pre-dividing and second separating; recoiling tension and recoiling speed are both adjustable.
- Hydraulic exit coil car — 15 t capacity, hydraulic lifting with 4 guide pillars, cycloid-motor traverse.
- Hydraulic system — hydraulic station, pipes and connectors serving all hydraulic units on the line.
- Electrical control system — frequency-conversion speed control for the whole line, centralized control. The main operation table provides high/low speed adjustment and manual strip feeding.
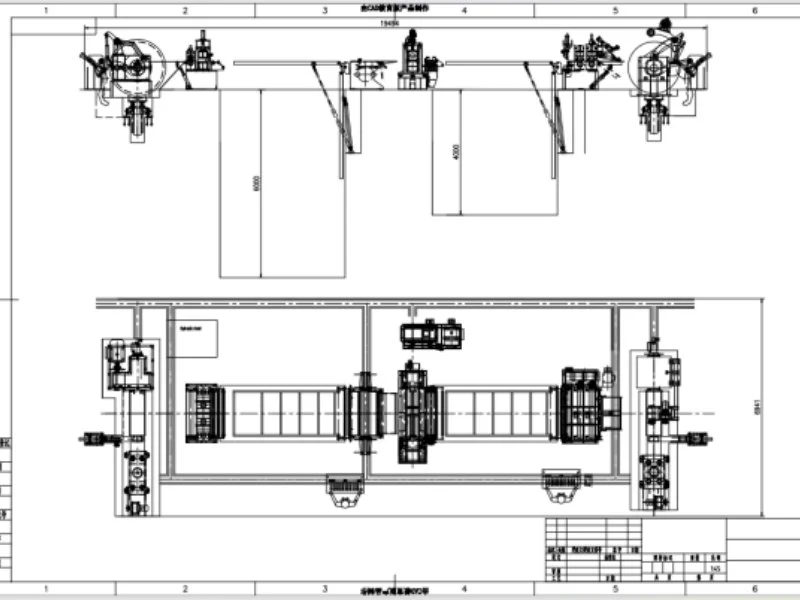 Overall line footprint: 23 m × 8 m.
Why Buyers Choose This Line
- Capacity that matches real production orders. A 1500 mm master coil becomes 15 strips at 1.5 mm, 10 strips at 2 mm, 7 strips at 3 mm or 6 strips at 4 mm, so a mixed-width order can be produced from a single master coil.
- Strip width accuracy of ±0.1 mm. Slitting accuracy is reinforced by side guides at both the centering unit and the slitter head, so the strip is positioned and held down during cutting.
- Active and pull shearing on one machine. The slitter switches between active shearing and pull shearing, giving you the right cutting mode for thick plate and for thin, high-accuracy strip.
- Recoil quality by design. The tension stand with pre-dividing and separating shafts builds tension with the 90 kW recoiler, and both recoiling tension and recoiling speed are adjustable — which is what produces tight, even coils.
- Heavy-duty coil handling at both ends. 15 t entry and exit coil cars with four-pillar hydraulic lifting, plus a hydraulic decoiler and recoiler both fitted with hydraulic supporting arms — no coil sag on the mandrel during processing.
- Part-processed coils recovered, not scrapped. The entry coil car can carry an unfinished coil back to the start position, so a job stopped mid-coil does not become waste.
- Coil set leveled before slitting. The pinch unit consists of 2 pinch rollers plus 5 leveling rollers, so the strip is leveled ahead of the slitter; the pinch rollers are lifted by motor and can also be adjusted by hand wheel.
- Cutting and splitting in one unit. The double-column hydraulic head cutter trims the coil head for clean entry into the slitter and also cuts a large coil into smaller coils, so you can split coils without a separate shear.
- Named component brands. SIEMENS PLC, Schneider low-voltage components and buttons, CHNT main electrical components, SINEE inverter, HUADE hydraulic valves, TAIXIANG reducers, DACHUAN AC motors, WEINVIEW/MCGS touch screen, HB/WB/LB bearings.
- Complete tooling package as standard. 20 LD slitting blades (Φ360 × Φ220 × 15 mm), 1 set of rubber rings, 2 pcs of woolen felt, 30 pieces of 45# separating plates (220 × 120 × 3), 45# shims (280 × 220 mm) from 0.95 mm to 100 mm, and PP big separation plates (150 × 120 mm) from 10 mm to 100 mm — a package sufficient for a 9-strip setup. More strips require extra blades and spacers to be purchased separately.
- Lean on manpower. 1 technician and 2 general workers run the line, with centralized control and a main panel featuring high/low speed adjustment and manual feeding.
- Delivered complete. Hydraulic station with pipework, electrical control, one set of installation tools, anchor bolts, lubrication equipment and the full operation instruction with electrical, hydraulic, layout and foundation drawings.
5. Technical Specifications
Maximum strips per coil (single pass)
Standard tooling supplied is sufficient for a 9-strip setup; for higher strip counts, additional blades and spacers should be purchased separately.
6. Line Composition
Main component brands
FAQ
Q1: How many strips can the line cut in one pass? Carbon steel: 6 strips at 4 mm, 7 at 3 mm, 10 at 2 mm, 15 at 1.5 mm. Stainless steel: 6 strips at 2–2.5 mm, 8 at 1.5 mm. The limit is set by coil thickness and material strength, not by the blade shaft.
Q2: What is the narrowest strip I can produce? Minimum finished strip width is more than 30 mm.
Q3: What materials and thicknesses are covered? Carbon steel 1.5–4 mm and stainless steel 1.5–2.5 mm, with tensile strength up to 450 MPa and yield strength up to 260 MPa. Master coil width 500–1500 mm, coil weight up to 15 t.
Q4: What is the width accuracy? Width tolerance is ≤ ±0.1 mm.
Q5: Which blades and tooling come with the machine? 20 pcs LD blades Φ360 × Φ220 × 15 mm, 45# separating plates 220 × 120 × 3 mm (30 pcs), 45# shims 280 × 220 mm from 0.95 mm to 100 mm, PP big separation plates 150 × 120 mm from 10 mm to 100 mm, plus 1 set of rubber rings and 2 pcs of woolen felt. This package supports a 9-strip setup; if you need more strips, extra blades and spacers should be purchased.
Q6: Does the line need a foundation pit? Yes. Two loop pits are required: Loop I 3500 × 2000 × 3500 mm and Loop II 4000 × 2000 × 5000 mm. Overall floor space required is 23 m × 8 m. We provide the foundation drawings; the buyer constructs and monitors the foundation, and the foundation holes are reserved for the machine foot bolts.
Q7: Which direction does the line run, and can it be reversed? The standard configuration runs from right to left with the operation table facing the machines. If your plant layout requires a different direction, inform us before production so we can adjust accordingly.
Q8: What is the delivery time and packing? 120 days. Shipped in 2 × 40 HQ + 1 × 20 GP containers. HS Code: 8462321000.
Q9: How many operators are needed? 1 technician and 2 general workers.
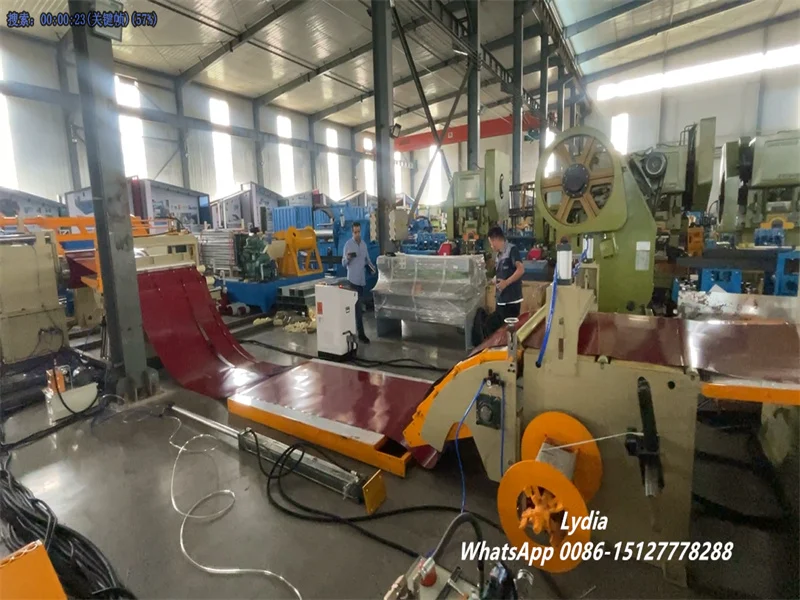
The metal coil slitting and recoiling machine is designed for processing narrow-width strips with high
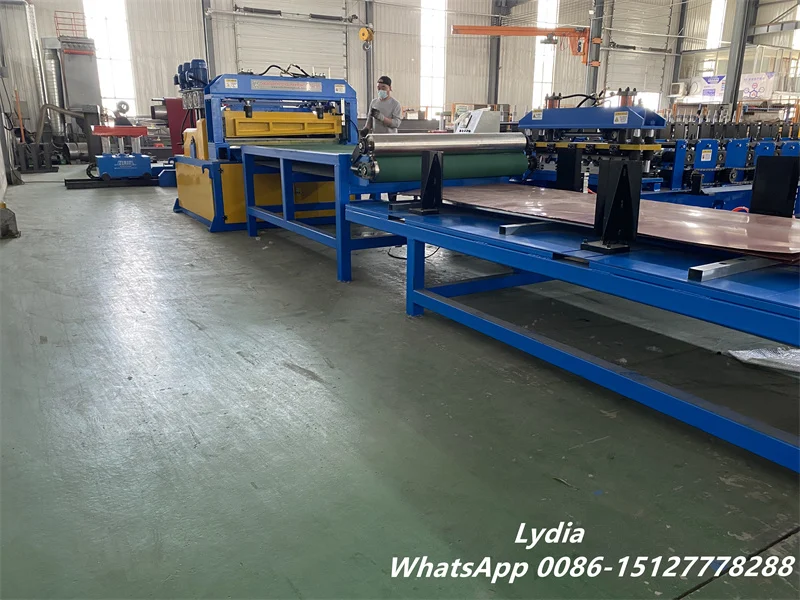
We are pleased to introduce our advanced slitting line solution, fully prepared for multi-material applications
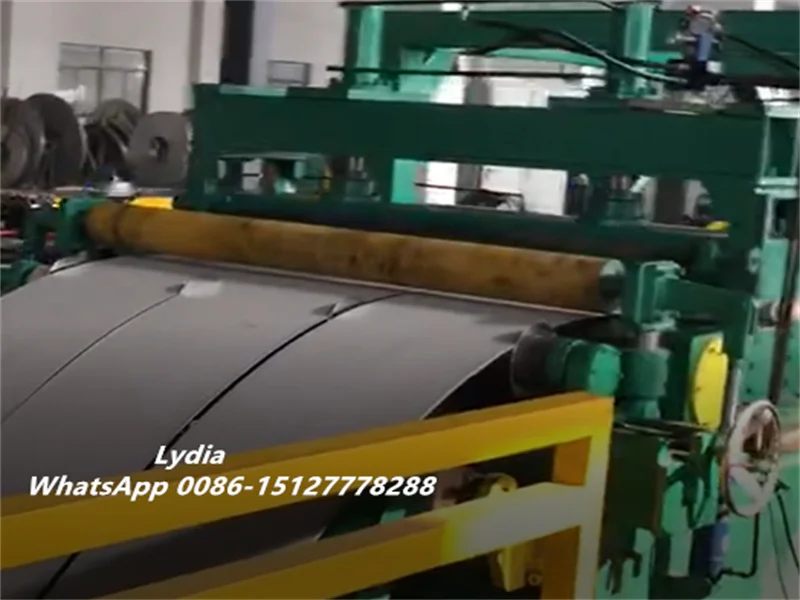
Main technical parameters for the High Speed Slitting Line Other parameters Power
-
Introducing our cutting-edge High-Speed Slitting Line—the ultimate solution for all your material slitting needs! Engineered
Why choose us?
Global Trust: Trusted By Customers In Over 156+ Countries And Regions, Our Roofing Sheet Making Machines Are Recognized For Their Outstanding Performance And Reliability Worldwide.