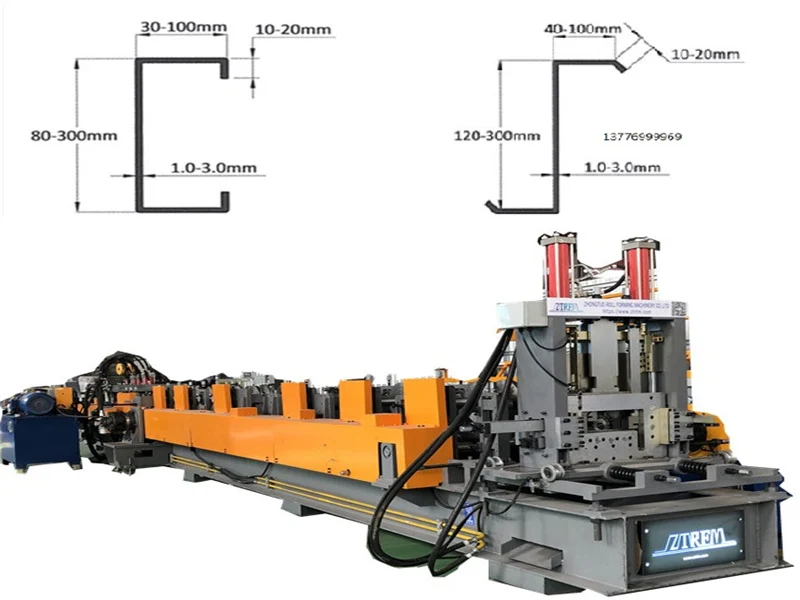
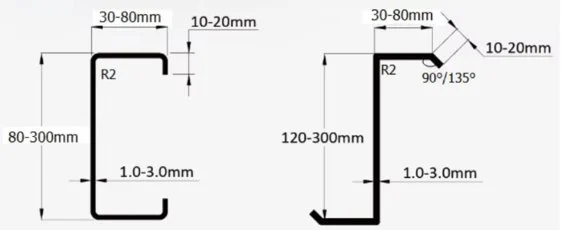
The CZ Purlin Roll Forming Line produces C and Z purlins from 1–3 mm steel coil, with size adjustment handled automatically through laptop control. C purlin web sizes run from 80 mm to 300 mm; Z purlin web sizes run from 120 mm to 300 mm. Punching runs in the line on two independent units — one for single holes, one for double holes — and the punching is done on the flat strip before forming. Two shears are fitted on the line: a pre-forming shear that cuts the punched flat strip to length ahead of the forming section, and a post-forming shear that cuts the formed purlin behind the forming section. Both cut methods are therefore available on one machine, without changing blades or reconfiguring the line between orders.
Because both punching units sit in the line, single-hole and double-hole purlins are produced in one continuous pass instead of two separate operations or a die change between patterns. Because punching happens before forming, the dies work on flat strip rather than on the closed profile. And because the size is entered on the laptop instead of being set by changing spacers and re-adjusting the roll stands by hand, a change from 80 mm to 300 mm web is a control-room operation.
Working Process
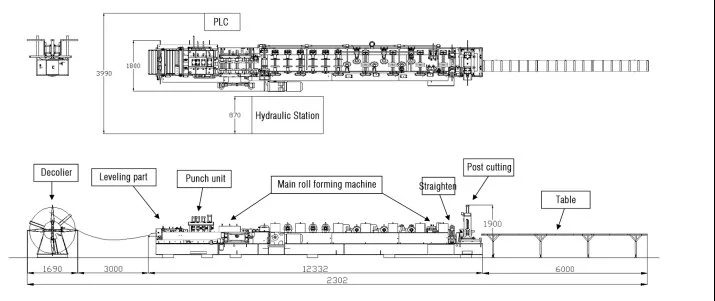
- Coil loading and uncoiling — hydraulic decoiler with coil car, coil weight up to 10 t, coil I.D.Φ 480 – 520 mm.
- Leveling — 4-roller leveler removes coil set so the strip enters punching flat and the hole pattern stays true.
- In-line punching (before forming) — two independent punching units work on the flat strip:
- Punching unit 1: single-hole punching;
- Punching unit 2: double-hole punching. Both units are mounted in the line ahead of the forming section, so either pattern is produced in the same pass without removing dies or re-setting the line.
- Pre-forming shearing — the punched flat strip is cut to length ahead of the forming section with a straight-blade shear. The cut end is square and no profile-shaped blade is needed; the forming section then receives strip already cut to the ordered length.
- Roll forming —18 forming stations roll the C / Z purlin section. Web (bottom) size: C purlin 80 – 300 mm, Z purlin 120 – 300 mm; material thickness 1 – 3 mm; flange and lip as per the customer drawing.
- Post-forming shearing — the formed purlin is cut behind the forming section with a profile-shaped blade. This shear works on the finished section, cutting the purlin to length and trimming the ends after forming.
- Run-out and discharge —run-out table / automatic stacker; purlins are discharged at 3 m length range for packing.
- Laptop automatic size adjustment — the operator enters the purlin size on the laptop and the line adjusts automatically. Size programs are stored, so repeating an earlier order is a program recall.
Why Buyers Choose This Line
- Two punching units in one line. Single-hole and double-hole patterns are punched by two dedicated units, so a purlin order that mixes both patterns runs without a die change between them and without a second handling of the material. This alone removes the punching press and the extra labour from the shops that order from you.
- Punching before forming — dies work on flat strip. Because punching is done ahead of the forming section, the dies press flat strip instead of a closed profile. The tooling is simpler and the hole pattern is generated before the section is formed.
- Two shears, two jobs, one line. The pre-forming shear cuts the punched flat strip to length with a straight blade — square ends, and no profile blade to make or re-grind. The post-forming shear cuts the formed purlin behind the forming section with a profile-shaped blade, working on the finished section. Both are fitted on the line, so flat-strip cut-to-length and formed-profile cutting are available from one machine without swapping blades or reconfiguring between orders.
- Size change by laptop, not by hand. The operator enters the size and starts the line; the automatic size adjustment removes the manual spacer and roll-stand setting from the changeover. Changeover between two sizes takes about 2 minutes, so short runs and mixed orders stay profitable.
- C 80 – 300 mm and Z 120 – 300 mm, 1 – 3 mm thick. One line covers both purlin types and the sizes a steel structure fabricator actually quotes, from thin 1 mm wall purlins to 3 mm heavy sections, instead of splitting orders across two machines.
- Continuous output, not batch output. Uncoiling, leveling, punching, forming, cutting and discharge run as one flow — purlins come off the line finished, ready for packing, and are never re-handled between a separate punch press and the roll former.
- Repeatable purlins order after order. Punching and forming parameters are stored per size program, so the first purlin of a re-run matches the last purlin of the previous run.
- Built for production, not for a demonstration. laptop control with program storage, 18 forming stations.
5. Technical Specifications
Purlin range (locked from your brief)
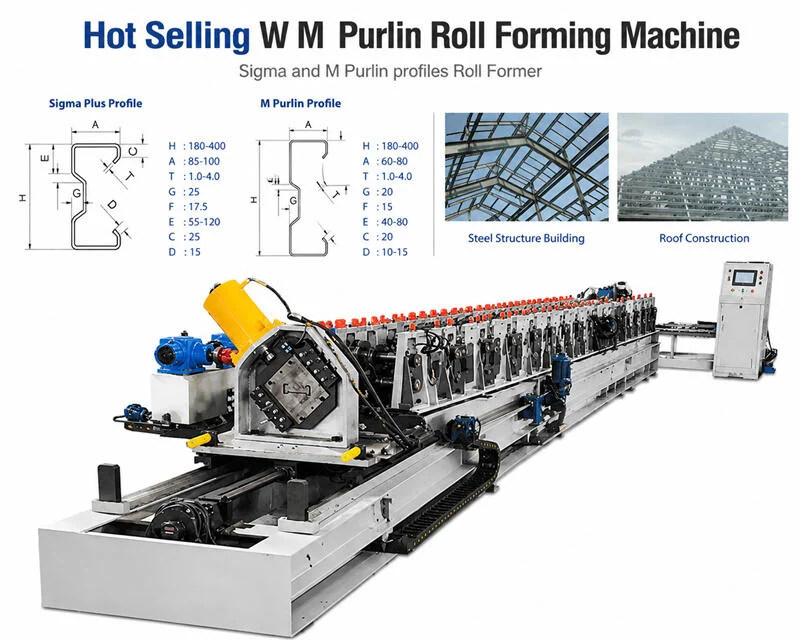
Regarding Sigma and M purlin profiles, we offer a tailored roll forming Method based on
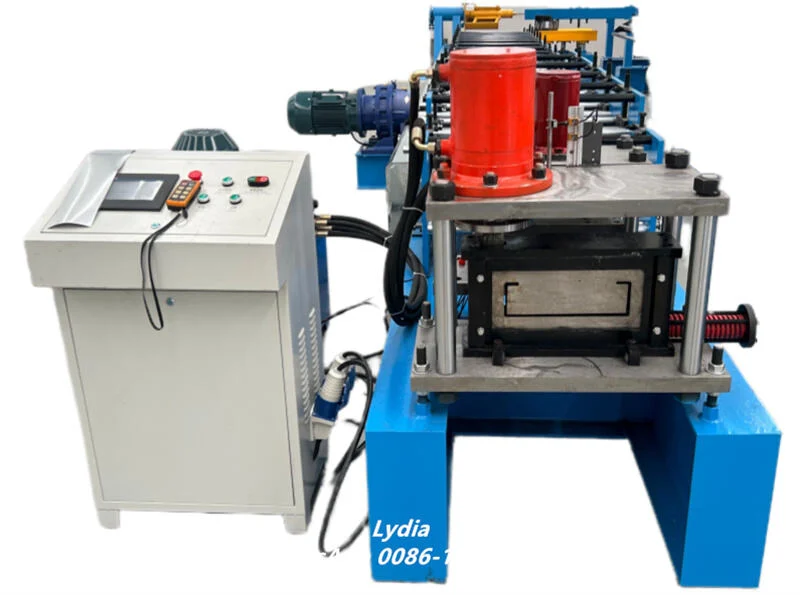
As the demand for prefabricated steel buildings continues to grow, manufacturers need production equipment that
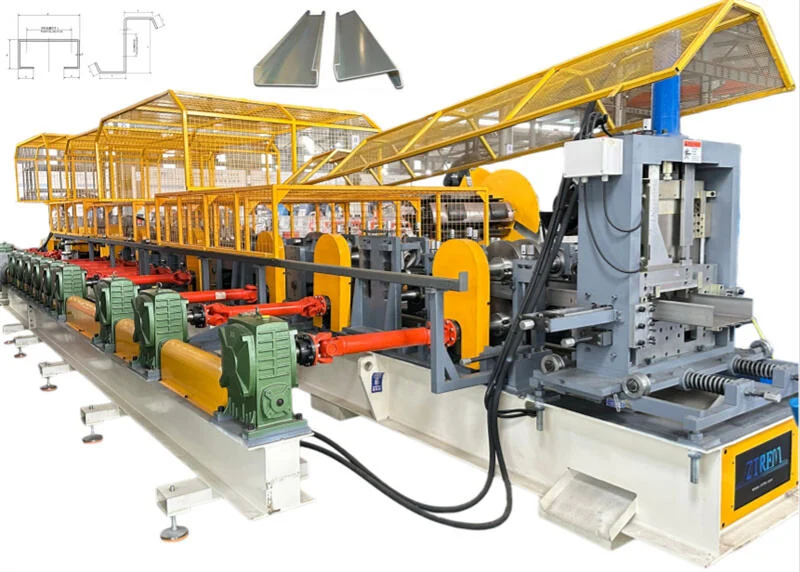
The demand for durable, lightweight, and cost-efficient structural steel continues to grow as industrial buildings,
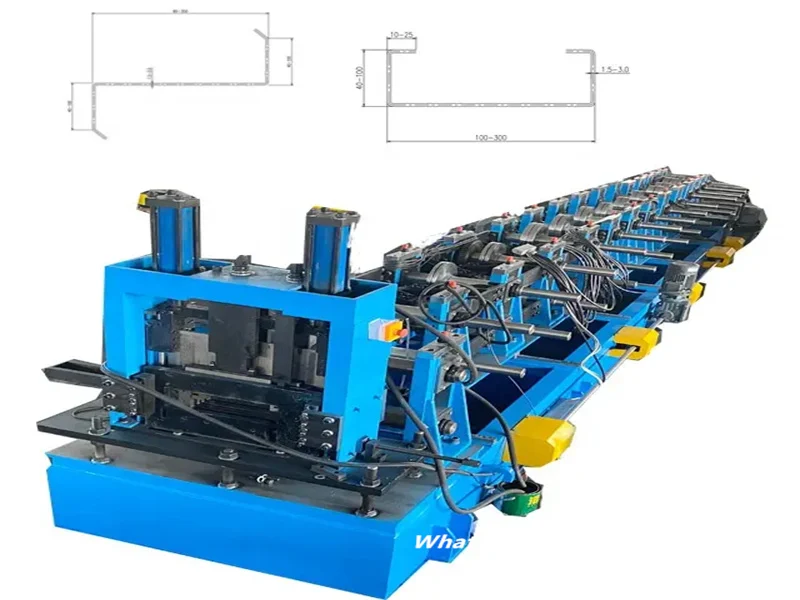
Professional C & Z Purlin Roll Forming Machine Heavy-Duty Automatic Machine for Structural Steel Production
Why choose us?
Global Trust: Trusted By Customers In Over 156+ Countries And Regions, Our Roofing Sheet Making Machines Are Recognized For Their Outstanding Performance And Reliability Worldwide.